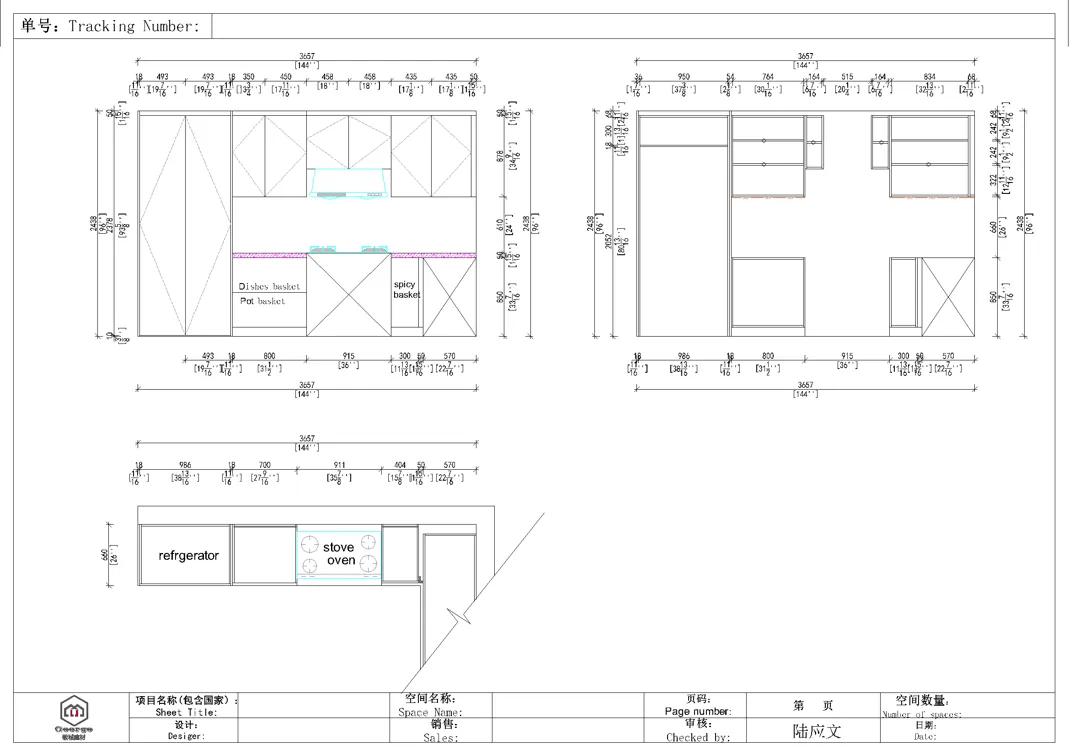
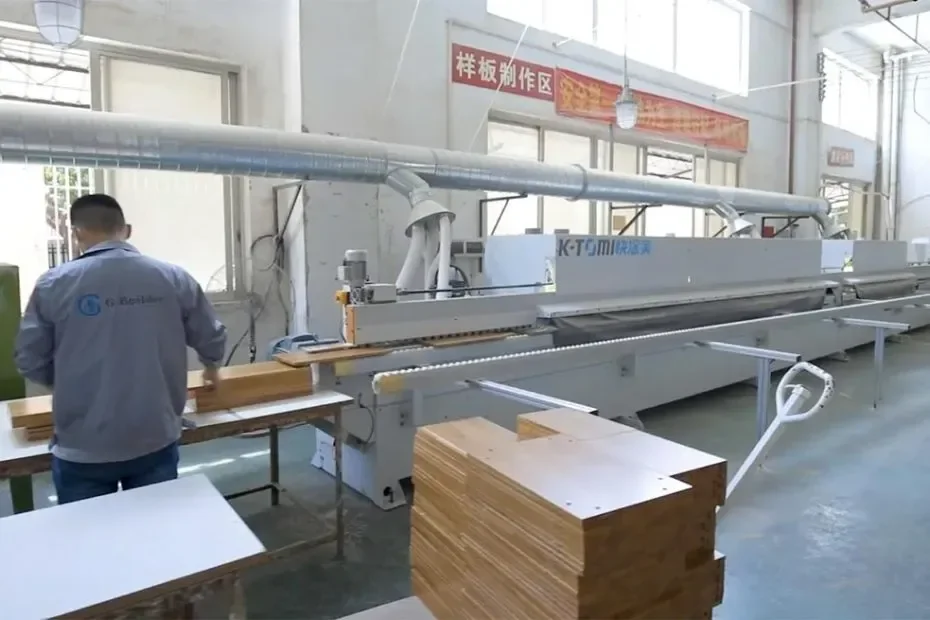
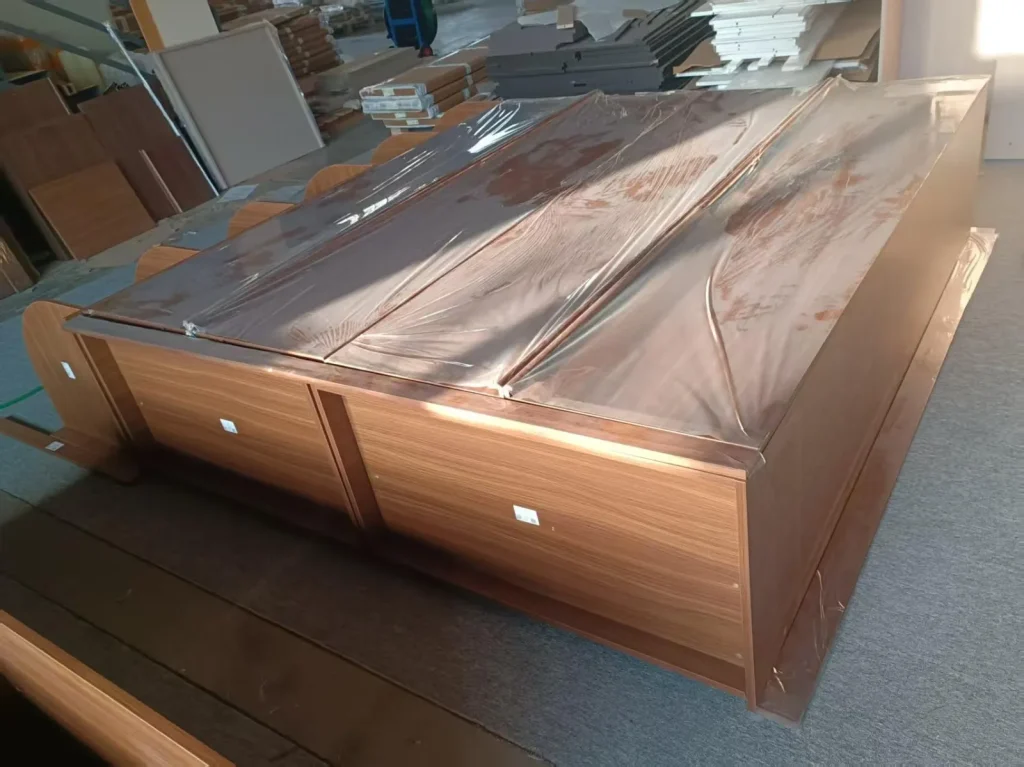
A useful quality plan connects the approved drawing and sample to measurable checks, issue handling, packaging and release. The GEORGE Group images below show cabinet drawing, workshop, protection and packing stages; they do not establish the responsible facility, date, standard or inspection record for a specific order.
Build a traceable control chain
- Approve the input: current room plan, cabinet elevations, material and hardware codes, appliance interfaces, samples and change record.
- Release production: identify the responsible facility, drawing revision, quantities, cabinet and room codes, and authorised release.
- Define inspection points: dimensions, visible finish, edge and joint condition, drilling, hardware operation, assembly, labelling and packaging as applicable.
- Record exceptions: describe the nonconformity, affected code, disposition, correction and recheck rather than relying on an informal message.
- Release and hand over: connect inspection status to the package list, loading record and site receipt.
Set approval and inspection points before production
| Control point | Record to request | Open decision |
|---|---|---|
| Drawing | Revision, approver, date and affected room or unit | What change requires reapproval? |
| Sample | Sample code, substrate, finish, hardware and accepted variation | Which rooms or cabinets does it govern? |
| In-process check | Item code, characteristic, result and inspector | Which checks are witnessed or reported? |
| Assembly or trial fit | Components checked, operating result and issues | Which cabinets require assembly before packing? |
| Final release | Quantity, finish, hardware, labels, package and issue closure | Who authorises shipment? |
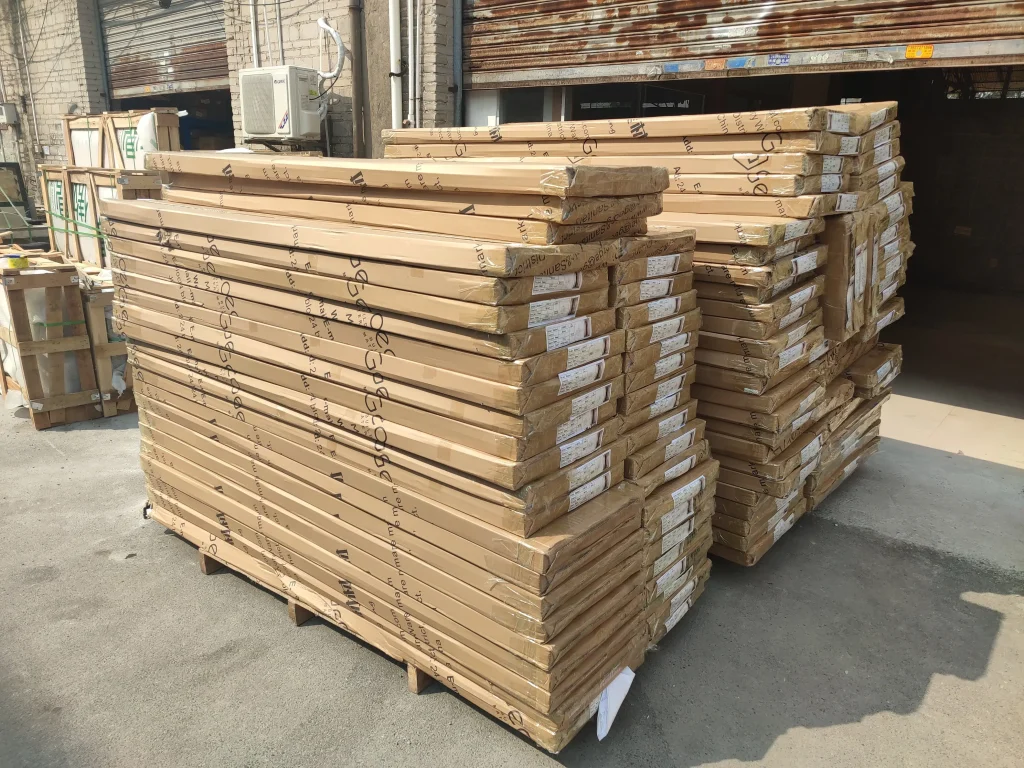
See the stages that a project quality plan must control
This GEORGE Group cabinet-factory tour provides visual context for material handling, machining, assembly and related workshop stages. It does not identify the production party, drawing revision, inspection standard or acceptance record for a proposed order.
Make deviations visible
A quality record should identify the cabinet or component, drawing revision, expected result, observed issue, decision, responsible person and recheck. The buyer should define which changes need written approval and what evidence is required before shipment.
These workshop images do not establish the standards, inspection staff, frequency, tolerances or production party for a specific order. Confirm them against the proposed package rather than inferring project-specific controls from general group media.
Define the records needed for your approval and handover
Send the cabinet scope, drawing and sample stages, measurable concerns, reporting format, packaging rules and any destination documents.